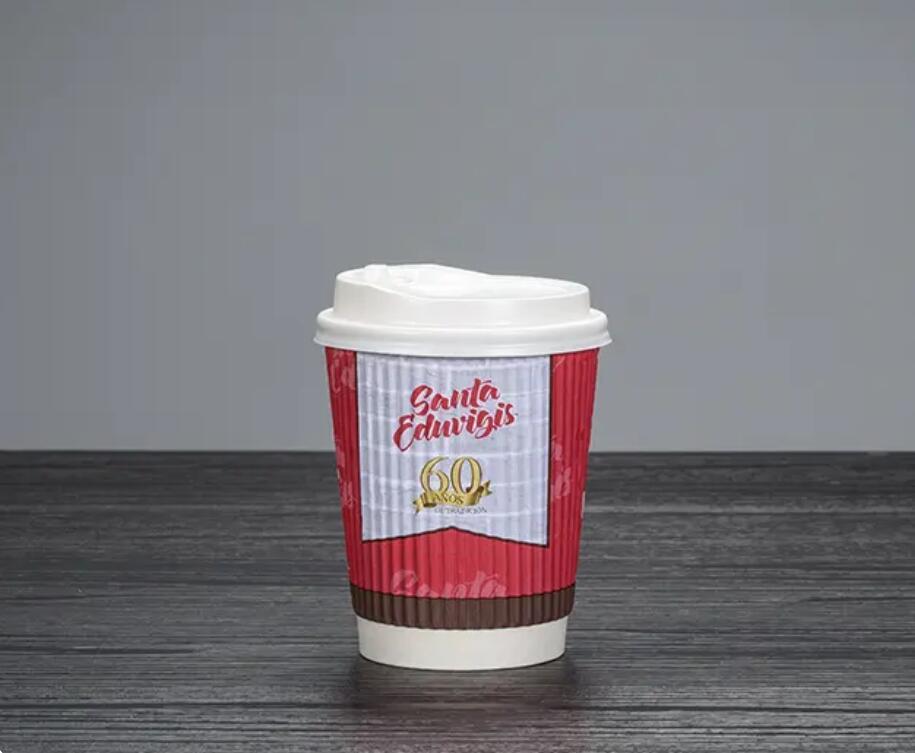
Designed primarily for food service operators, cafes, and hospitality providers, the 8oz Ripple Wall Paper Cup addresses critical needs for beverage containment with improved heat resistance and usability. Our company, among leading paper cup manufacturers, provides this solution targeting operational workflows requiring disposable paper cups that facilitate hot and cold beverage serving with consistent quality. This product suits entities sourcing wholesale paper cups that demand compliance with food safety standards and supplier reliability in bulk procurement scenarios.
This disposable paper cups solution integrates a unique ripple wall design that enhances insulation performance while offering improved tactile grip for operators handling hot or cold liquids. Constructed with food-grade paper combined with PE, PLA, or aqueous coatings, the cup sustains structural integrity under thermal stress. Dimensions include a height of 90mm and an 80mm diameter, supporting a 8oz capacity. Packaging logistics accommodate 25 pcs per pack in cartons of 20 packs, enabling efficient inventory and supply chain handling, essential for wholesale paper cups operations.
In various professional environments such as chain cafes, catering services, and event management companies, the ripple wall cup functions as a key component for disposable paper cups usage. Its environmental certifications support compliance with sustainability policies within food service sectors. The cup integrates seamlessly within packaging and dispensing systems, contributing to operational efficiency and brand presentation. paper cup suppliers leveraging this product can fulfill corporate accounts requiring large-scale supply while ensuring customer safety and regulatory adherence.
This model incorporates a ripple wall architecture that strategically dissipates heat, reducing the risk of user discomfort, an improvement over traditional smooth-sided paper cups. The food-grade paper stock paired with PE, PLA, or aqueous coatings ensures durability across temperature variations while maintaining recyclability and environmental compliance. Such design advances by paper cup suppliers reinforce product consistency and adaptability for wholesale paper cups distribution channels seeking modular packaging solutions.
Users engaging with these disposable paper cups benefit from enhanced thermal insulation and ergonomic handling characteristics, supporting both hot beverage safety and cold drink condensation management. The ripple texture mitigates slip risk during transport and reduces the need for additional sleeves or carriers. For paper cup manufacturers and wholesale paper cups vendors, this translates into a cost-effective, scalable product that aligns with sustainable packaging trends while preserving user convenience.
|
Item |
Spec.(mm) |
Raw material |
ctn size |
package |
|
4oz |
62*46*64 |
210g+15gPE/PLA/Aqueous+240g |
43*33*26 |
25pcs*20pks |
|
6oz |
73*49*80 |
210g+15gPE/PLA/Aqueous+240g |
38*31*37cm |
25pcs*20pks |
|
8oz |
80*56*90 |
280g+18gPE/PLA/Aqueous+240g |
46*40*33cm |
25pcs*20pks |
|
10oz |
90*60*94 |
300g+18gPE/PLA/Aqueous+240g |
42*45*36 |
25pcs*20pks |
|
12oz |
90*60*110 |
300g+18gPE/PLA/Aqueous+240g |
45*45*36cm |
25pcs*20pks |
|
16oz |
90*60*135 |
300g+18gPE/PLA/Aqueous+240g |
55*45*36cm |
25pcs*20pks |
|
20oz |
90*64*150 |
300g+18gPE/PLA/Aqueous+240g |
72*45*37cm |
25pcs*20pks |
Within high-demand catering environments and food service chains, disposable paper cups with ripple wall construction function as essential supply items facilitating hot and cold beverage distribution with operational efficiency. The cups’ insulation reduces beverage temperature loss, improving service quality. Their compliance with food safety standards and bulk packaging configurations integrate effectively within procurement and inventory management systems managed by paper cup manufacturers and suppliers.
Establishments emphasizing environmentally responsible packaging benefit from offering these disposable paper cups as part of their branding and customer engagement strategy. Customized options from paper cup suppliers allow alignment with corporate design standards while meeting demand for wholesale paper cups that are certified and compliant. In such scenarios, the cups serve as touchpoints reinforcing eco-friendly values and operational workflows aligned with circular economy principles in food packaging systems.
What materials are used in your 8oz Ripple Wall paper cups?
We manufacture the 8oz Ripple Wall paper cups using food-grade paper combined with PE, PLA, or aqueous coatings. These materials are certified safe and eco-conscious, aligning with our commitment to providing high-quality disposable paper cups suitable for hot and cold beverages.
Can I customize the design of the 8oz Ripple Wall Paper Cup to match my brand?
Yes, we welcome customization to help you promote your brand effectively. Our production supports custom-printed designs on these paper cups to meet your specific branding requirements, perfect for cafes, restaurants, or large-scale food service operations.
What is the typical lead time and minimum order quantity for wholesale paper cups?
Our standard lead time ranges from 15 to 25 days, with a minimum order quantity of 30,000 pieces per size. We package these wholesale paper cups efficiently in bulk to ensure smooth logistics and supply chain management for your business.
How do you ensure the quality and safety of your paper cup products?
We adhere to strict quality control, backed by certifications such as BRC, SGS, ISO, and FSC. Our materials are food-grade and comply with relevant standards, ensuring our paper cup manufacturers provide safe and reliable products for your beverage service needs.